When manufacturers and converters ask, “what is the shelf life of metallized PET film,” the answer is rarely a single date. Many suppliers recommend using unopened rolls within 12 to 24 months. However, the technical data sheet and certificate of analysis should guide the final decision. Storage conditions can change the result significantly.
A stable warehouse should remain cool, dry, and clean, with limited sunlight and controlled humidity. Avoid direct floor contact. Keep rolls sealed in their original packaging until production. Heat, moisture, dust, and repeated temperature changes may weaken adhesive performance or reduce surface quality. A roll stored beside a loading door may age faster than one kept in a controlled room.
Check it carefully.
Before printing, laminating, or coating, inspect the roll for oxidation, telescoping, blocking, edge damage, and uneven winding. Test metal adhesion, surface tension, optical density, and bond strength against the original specification. These tests provide stronger evidence than the calendar alone. In practical production, film beyond its recommended period may still perform well, while poorly stored newer film may fail.
That distinction matters.
Records also improve reliability. Note the manufacturing date, lot number, storage temperature, and opening date. Contact the original manufacturer when the packaging is damaged or the film shows unusual discoloration. This article examines realistic shelf-life expectations for 2026, but it does not replace supplier validation. Shelf life is a useful estimate, not a promise. My own cautious view is simple: test every questionable roll before committing it to a full production run.
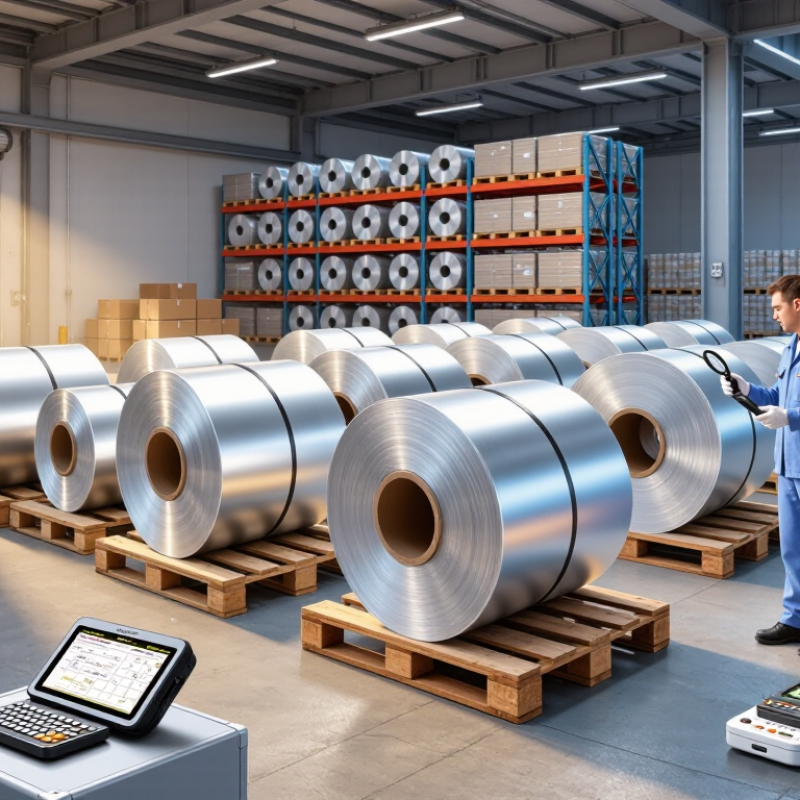
In 2026, shelf life for metallized PET film means more than a printed date. It describes how long the film should retain usable barrier, appearance, adhesion, and converting performance under defined storage conditions. A practical specification should state temperature, humidity, packaging, and inspection intervals. Without those details, “24 months” can be misleading. It is a planning estimate, not a guarantee.
From a converter’s perspective, unopened rolls need controlled, dry storage away from sunlight, dust, and heat sources. Keep rolls in their original wrapping until conditioning begins. Sudden temperature changes may create condensation. That small mistake can affect winding, corona treatment, coating adhesion, or printing consistency. In 2026, quality teams increasingly use batch records and periodic checks to connect storage history with actual performance. Test a retained sample near the end of the stated period. Check haze, metal adhesion, surface energy, blocking, and tensile behavior.
Do not rely on appearance alone. A shiny surface may hide weakened adhesion or reduced barrier performance. Film stored beyond its recommended period is not automatically unusable, but it needs documented evaluation before production. Results can vary between structures, thicknesses, and metallization levels. Storage assumptions are sometimes treated as facts. That is where preventable waste begins. A conservative, evidence-based approach works better, especially when test data challenges the original shelf-life estimate.
| Data Dimension | Practical 2026 Guideline | Why It Matters | Recommended Control or Check |
|---|---|---|---|
| Unopened roll shelf life | Typically up to 12 months from the manufacturing date when the roll remains sealed in its original protective packaging and is stored under controlled conditions. | Metallized PET film can gradually lose process consistency because of aging, moisture exposure, surface contamination, blocking, or changes in coating and adhesive behavior. | Use the manufacturing date and lot records for stock rotation. Confirm the exact limit in the applicable technical data sheet. |
| Storage temperature | Approximately 15–30°C is a common controlled-storage range; avoid prolonged exposure to high heat, freezing conditions, and rapid temperature changes. | Temperature extremes can increase roll deformation, condensation risk, telescoping, blocking, and dimensional instability. | Store indoors in a clean, dry area and allow cold rolls to reach room temperature before opening. |
| Relative humidity | Approximately 40–60% RH is generally suitable for storage, unless the product specification states otherwise. | Excess humidity can promote condensation and affect adhesive, ink, coating, and lamination performance. Very dry conditions can increase static and handling problems. | Monitor warehouse humidity and never open protective packaging while condensation is present. |
| Protection from light | Keep away from direct sunlight and strong UV exposure. | Light and heat can accelerate aging of packaging materials, coatings, adhesives, and printed structures, even though the aluminum layer itself is not normally the main aging concern. | Keep rolls in opaque or light-resistant packaging and away from windows, heaters, and outdoor storage. |
| Original packaging | Keep sealed until use; protective wrapping, end caps, and core protection should remain intact. | The metallized surface and film edges can be damaged by dust, abrasion, moisture, and incorrect handling. | Inspect packaging for tears, punctures, water marks, crushed edges, or loose wrapping before accepting the roll. |
| Opened-roll handling period | Use as soon as practical, preferably within several days to a few weeks, depending on humidity, packaging quality, and process sensitivity. | After opening, the film is more exposed to dust, moisture, static, edge damage, and surface contamination than an unopened roll. | Reseal unused material with moisture-resistant packaging and record the opening date. |
| First-in, first-out control | Use FIFO stock rotation and prioritize rolls approaching 12 months of age. | FIFO reduces the risk of unplanned aging and makes traceability easier when several production lots are stored together. | Label each roll with manufacturing date, opening date, lot number, and storage status. |
| Appearance after storage | Acceptable rolls should generally be free from visible corrosion, severe wrinkles, blocking, telescoping, crushed edges, excessive dust, and abnormal discoloration. | Visible defects can cause web breaks, print defects, poor lamination, uneven sealing, or reduced barrier performance. | Perform a visual inspection under suitable lighting before production release. |
| Optical performance | Check metallized appearance, gloss, haze, optical density, and transparency against the approved product specification. | Optical changes may indicate surface damage, oxidation, coating problems, or nonuniform metallization. | Compare retained samples or approved reference values using calibrated test equipment where required. |
| Barrier performance | Verify oxygen and water-vapor barrier values when the film is used for sensitive packaging applications. | Barrier performance depends on film structure, metallization quality, coatings, flexing, lamination, and storage history; visual appearance alone cannot confirm it. | Test oxygen transmission rate and water-vapor transmission rate according to the relevant product specification and laboratory method. |
| Mechanical and dimensional stability | Check tensile behavior, elongation, thickness, width, curl, and web flatness when the roll is near or beyond its recommended storage period. | Aged or poorly stored film may show handling problems, registration variation, wrinkles, or higher break frequency. | Run a controlled trial or laboratory inspection before releasing older stock for critical production. |
| Lamination and adhesive compatibility | Requalify before critical use if storage exceeds the stated shelf life. | Surface treatment and adhesive interaction can change over time, affecting bond strength, curing, delamination resistance, and package integrity. | Perform a lamination trial and measure bond strength after the specified conditioning or curing period. |
| Printing and coating suitability | Confirm ink wetting, coating adhesion, surface energy, and print appearance before full-scale production. | Surface contamination, aging, or reduced treatment effectiveness may cause poor wetting, pinholes, smearing, or adhesion failure. | Use surface-energy checks and an application-specific print or coating trial. |
| Material beyond the recommended shelf life | Do not automatically scrap or release; quarantine and evaluate the roll first. | Shelf life is a recommended quality period, not a guarantee that the material fails immediately afterward. Suitability depends on storage history and end use. | Obtain technical approval and complete visual, dimensional, adhesion, and barrier checks before use. |
| Expected service life in a finished product | Not the same as roll shelf life. Finished-product life may range from months to years depending on the complete package structure and application. | Temperature, humidity, ultraviolet exposure, flexing, chemicals, seal quality, and the other laminated layers can control the final product lifetime. | Use application-specific accelerated aging and real-time shelf-life testing rather than relying only on the film roll’s storage period. |
| Release decision for 2026 production | Release only when storage records and performance checks are acceptable. | A calendar date alone cannot confirm suitability for food, pharmaceutical, industrial, or decorative applications. | Follow the current technical data sheet, quality plan, regulatory requirements, and customer-approved specifications. |
| Important: The 12-month figure is a practical planning guideline commonly used for unopened metallized PET film under controlled storage, not a universal guarantee. Actual shelf life varies with film construction, metallization, coatings, surface treatment, packaging, storage conditions, and intended application. Always verify the current specification and test older material before production use. | |||
Properly stored rolls may remain usable for 6–24 months. It depends. Film structure, packaging, humidity, and handling history all matter.
Keep unopened rolls indoors at 20–25°C. Maintain approximately 40–60% relative humidity. Protect rolls from sunlight, heaters, condensation, and sudden temperature changes.
Keep each roll in its original moisture-resistant wrapping. Store rolls upright on clean supports. Protect their edges from impacts. Do not stack heavy materials on top.
Oxygen and moisture may reduce the metal layer’s reflectivity. Heat accelerates this change. The surface may appear dull before performance clearly declines.
Yes. Cold rolls can develop condensation when moved into warm air. Allow them to acclimatize for at least 24 hours before opening. Moisture may affect printing or adhesive bonding.
Check for scratches, edge damage, telescoping, blocking, and excessive winding pressure. Small defects can reduce barrier performance. Forklift contact may leave problems that are easy to miss.
Examine the outer, middle, and inner roll layers. Check appearance, adhesion, optical density, and surface friction. Test oxygen and water vapor barrier performance when needed. A clean surface proves little.
Not always. A twelve-month rule is useful, but it cannot guarantee performance. A roll may look acceptable yet bond poorly during production. Laboratory evidence and current inspection results provide better guidance.
The question “what is the shelf life of metallized PET film” depends on its structure, coating quality, packaging, and storage environment. In 2026, properly manufactured and stored metallized PET film may remain suitable for use for several years, but its performance can gradually change over time. Exposure to heat, humidity, oxygen, light, dust, and chemical vapors may weaken adhesion, reduce barrier properties, cause surface oxidation, or create wrinkles and discoloration. The film’s intended application and required performance standards should also be considered when defining its usable life.
For longer stability, store the film in its original sealed packaging in a clean, dry, and well-ventilated area away from direct sunlight and heat sources. Avoid sudden temperature changes, excessive stacking pressure, and contact with moisture or contaminants. Before use, inspect the roll for damaged packaging, telescoping, blocking, unusual odor, surface defects, or changes in metallization. If necessary, test adhesion, appearance, and functional performance on a small sample before production.
 Benchmark Plastic